
 Business License
Supporting Tube Producers With Scraper Blade Development
1. Why Scraper Blade Development Support Starts With the Mill's Line
Scraper blade development support starts with a question that has nothing to do with carbide. It starts with what the line is doing: the tube size, the wall, the bead height, the line speed and the state of the mill. A blade that performs on one line and not on another is usually a blade that was developed against the wrong set of those figures.
The reason is that a scraper blade cuts a bead that is still forming and still hot. The edge does not meet a stable workpiece. It meets a ridge whose height varies along the seam and around the circumference, on a tube that is not yet round, at a speed that gives the edge a fraction of a second per metre. The line is the specification.
Serving as a tube producer tooling partner means working on the mill's figures rather than on a catalogue, and Winray New Materials works with tube producers on custom scraper trial programmes for that reason, and the pattern that has come out of those programmes is consistent. The mills that get to a working profile quickly are the ones that can describe their line in numbers before the first blade is ground.
2. What a Tube Producer Tooling Partner Brings to a Trial
A tube producer tooling partner brings two things that a catalogue supplier does not. The first is a blade ground to the mill's own figures rather than to a size range. The second is a reading of the failed blade, because the wear pattern on a returned blade says more about the line than the mill's description of it does.
What a tube producer tooling partner adds is a reading rather than a part, and the reading is the part that changes the outcome. A blade that has worn evenly along the land tells a different story from one that has worn at the corners, and the two lead to different edge angles. A blade that has chipped at the trailing corner points at the alignment rather than at the material, and no change of grade corrects an alignment fault.
Winray New Materials Co Ltd grinds trial blades against the mill's schedule and reads the returned blade against the same schedule, so the two halves of the programme use one set of figures. A trial that is quoted in nominal diameters and read in measurements is a trial with two specifications in it.
3. Custom Scraper Trial: The First Blade Is a Measurement
A custom scraper trial is not a demonstration, and the first blade is not there to prove that the tool works. It is there to measure how the line behaves when a blade is presented to it, and the useful output is a set of figures rather than a verdict.
The first blade is normally ground at the centre of the calculated band for the mill's wall, with an edge angle in the middle of the range and an interference that the wall can support. That is a starting point rather than an answer. The blade then runs for a defined period, and the mill records what happened rather than whether it liked the result.
The distinction matters because a first blade that performs well can hide a line that is on the edge of its window. A blade that runs at the centre of the band and shows even wear is a blade that confirms the calculation. A blade that runs well but shows corner wear is a blade that is telling you the mill is not aligned to the seam.
4. What the Mill Records During a Custom Scraper Trial
What the mill records during a custom scraper trial decides whether the second blade is better than the first. The record has to cover the line as it ran rather than as it was set, because the two differ more often than mills expect.
The minimum set is the tube size and wall actually run, the line speed, the bead height measured on a sample, the kilometres run on the blade, and the bore condition behind the cut. The bore condition is the figure most often left out and the one that shows a blade that is cutting into the parent metal rather than into the bead.
The table sets out the record against the decision it supports, because a record nobody uses is a record that stops being kept.
| Recorded figure | What it supports | What it catches |
|---|---|---|
| Tube size and wall as run | Interference setting for the next blade | A schedule change during the trial |
| Line speed | Edge angle and grade | A speed the edge cannot carry |
| Bead height on a sample | Depth of cut | A weld that is running high or low |
| Kilometres on the blade | Service interval | A blade being changed on a calendar |
| Bore condition behind the cut | Whether the cut is in the bead | The edge reaching the parent metal |
5. Reading a Custom Scraper Trial Blade Back to the Drawing
Reading a trial blade back to the drawing is the step where most of the learning happens, and it has to be done with the blade in hand rather than from a description. The four readings that matter are the land width, the wear distribution along the edge, the condition of the corner, and whether the wear is on the edge or behind it.
A land that has widened evenly across the whole edge is a blade that was set correctly and has worn to the end of its interval. A land that has widened at one end is a blade that met an alignment fault. A land that has widened in the middle and not at the ends is a blade that met a bead that was crowned, which is a weld problem rather than a tool problem.
Wear behind the edge is the reading that is easiest to miss. A blade that has lost material on the body behind the land has been running with too little clearance, and the correction is a geometry change rather than a grade change. Winray reads that pattern on returned blades more often than any other, and it usually appears on lines that have been chasing a burr by adding interference.
6. From Custom Scraper Trial to Repeat: What Changes in the Second Blade
From trial to repeat, the second blade changes in one or two figures rather than in its design. A trial that came back with even wear and a short interval gets a harder grade or a slightly larger edge angle. A trial that came back with corner wear gets a change to the alignment advice before the geometry is touched.
The discipline is to change one figure at a time, because a second blade that changes three things cannot be read. A mill and a supplier that change the edge angle, the interference and the grade together learn nothing from the second trial and usually end up back at the first.
The case that shows the value of one change at a time came from a mill running 48 mm tube some time ago. The first blade ran 900 kilometres and showed a worn land with corner chipping. The second blade changed the edge angle and nothing else, from 70 to 62 degrees, and ran 1,400 kilometres with an even land. The third blade added a grade change and reached 1,900 kilometres, which is the profile the mill still runs.
A mill that sent a drawing without a cut section some time ago received a first blade set to the schedule rather than to the bead. The blade removed most of the bead and left a fin along one side, because the weld was running high on that line. A section sent with the second enquiry showed the fin, and the interference went up by 0.08 mm on the third blade, which cleared it.
7. Where Scraper Blade Development Support Stops
Scraper blade development support stops at the edge of the blade, and saying so is part of being useful. A supplier can change the geometry and the grade. A supplier cannot align a mill, correct a weld that is running cold, or fix a holder that has lost its adjustment.
Scraper blade development support has to hold that line, because a programme that is asked to solve a mill problem will produce a series of blades that each fail differently. If the trial blade shows an uneven land and the mill is not aligned to the seam, the next blade will show the same thing whatever is changed inside the tool.
Winray New Materials states that boundary at the start of a programme rather than at the end of a third trial. A mill that knows what the supplier will not change spends its trial time on the variables that can move, and the programme reaches a working profile in fewer iterations.
8. What a Mill Brings to a Custom Scraper Trial
What a mill brings to a custom scraper trial decides how many iterations the programme takes, and a tube producer tooling partner works with what the mill supplies. The four inputs are the tube schedule, the line speed range, the current blade drawing with whatever is known about its performance, and access to a section of tube that the line has run.
The current blade drawing is the input that mills undervalue. A drawing that shows the edge angle and the interference the line has been running is a record of what has already been tried, and a programme that starts without it repeats work that has already been done. A drawing that is missing is itself information, because it means the blade has been bought on a size rather than on a specification.
Winray New Materials Co Ltd asks for a cut section of tube as well, because the bore behind the cut shows whether the current blade is removing the bead or reaching past it. A mill that sends a section with the enquiry gets a first blade that is closer to the answer than one that sends a drawing alone.
9. Frequently Asked Questions on Scraper Blade Development Support
9.1 How long does a custom scraper trial take from first enquiry to a working profile?
Three blades is the usual count, and the time is set by how fast the mill can run each one rather than by the grinding. A first blade ground to the centre of the calculated band goes out within a normal lead time. The second follows the reading of the first, and the third usually settles the profile. A programme that reaches a working profile in two blades is a programme where the mill's inputs were complete at the start.
9.2 What does a tube producer tooling partner need from the mill before the first blade?
The tube schedule, the line speed range, the current blade drawing and a cut section of tube. The schedule and the speed set the geometry. The drawings show what has already been tried, which is worth as much as the figures they contain. The cut section shows whether the blade in service is removing the bead or reaching into the parent metal, and that reading changes the interference on the first blade, which is why a mill that sends all four gets a first blade closer to the answer.
9.3 Why does a trial blade wear unevenly along the edge?
Because the bead is not uniform and the mill is not aligned to it. A bead that is crowned wears the middle of the land, a head that is offset from the seam wears one end, and a tube running oval wears the blade where the wall is thinnest. None of those is corrected by a grade change, and the useful response is to measure the bead and check the alignment before the second blade is ground. A worn land that is even is a blade set correctly and run to its interval.
9.4 Can a scraper blade development programme fix a burr that comes from the weld?
No, and a programme that is asked to do it will produce a series of blades that each fail differently. A weld running cold produces a bead that is hard and irregular, and a blade that meets it wears at the corners whatever its geometry. The correction belongs to the weld. A blade can be ground to survive a poor bead longer and cannot make a poor bead into a good one, so the useful question before a trial is whether the bead is consistent, because a consistent bead can be tooled around and an inconsistent one cannot.
Recently Posted
-
Carbide Punch Pins in Progressive Die Piercing of Sheet Metal
November 18, 20261. Progressive Die Punch Pin Loads at 300 Strokes a Minute A progressive die punch pin does not do one job. It does the job of its Read More
-
How to Order Custom Carbide Punch Pins From a Drawing
November 17, 20261. Why a Punch Pin Drawing Carries More Than a Part Number A part number describes a pin that already exists. Beyond the standard
Read More -
Solid Carbide Punch Pin vs Coated Punch: Which Holds Diameter Longer
November 17, 20261. Why a Solid Carbide Punch Pin and a Coated Punch Are Compared Wrong A solid carbide punch pin is usually compared with a coated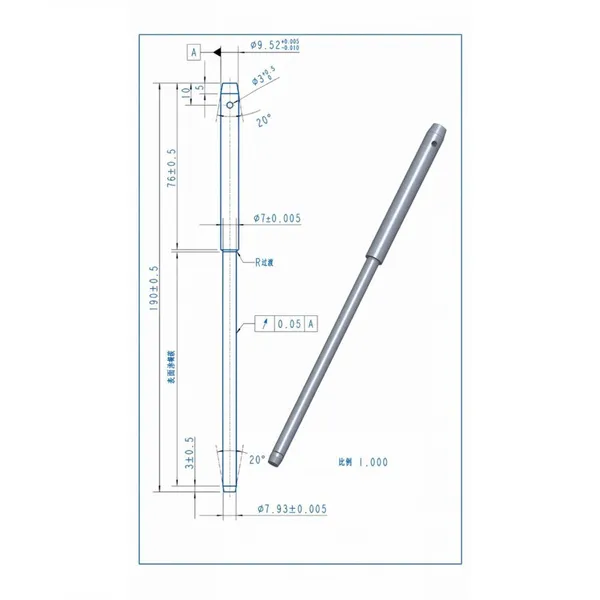 Read More
-
Carbide Punch Pin vs HSS Punch: Wear Life per 100,000 Strokes
November 17, 20261. Why Punch Cost per Stroke Is a Better Question Than Pins per Year A terminal stamper a while back asked us to quote a punch pin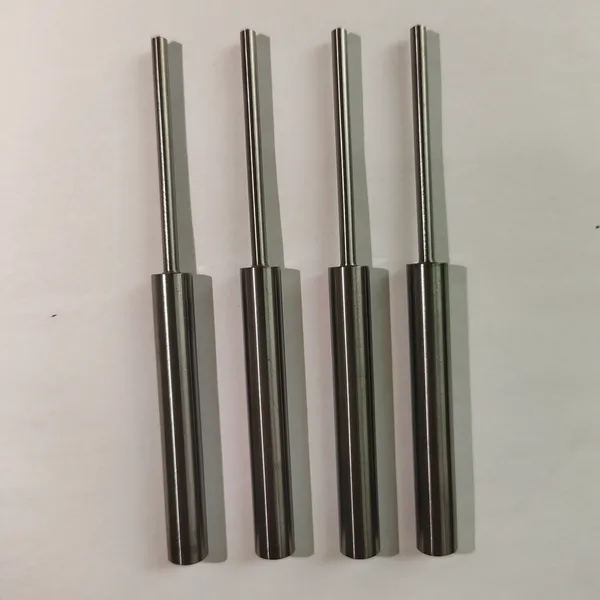 Read More

Contact Us
Recommended Products
-
 Non-Magnetic Nickel-Bonded Cemented Carbide Molds, Submicron Grain, Mirror Polished CavitiesNegotiableMOQ: 1 Blade
-
Non-Magnetic Carbide Grades for Specialized MoldsNegotiableMOQ: 1 Unit
-
Tungsten Carbide Punches HRA 90.5 Co 10% +/-0.002 mm Tolerance Mirror-Polished for Stamping DiesNegotiableMOQ: 1 Unit
-
Custom Carbide Strips and Round Blanks With 0.05mm Flatness for Machine ToolingNegotiableMOQ: 1 Unit
-
Custom Cemented Carbide Blanks ISO Standard Compliant With Ra 0.4 Surface FinishNegotiableMOQ: 1 Unit
-
Precision Ground Carbide Inserts and Blanks – Custom Grades and Tolerances up to ±0.01mmNegotiableMOQ: 1 Unit
-
Ground Carbide Rods Ø8mm x 200mm, h6 Tolerance, Ra 0.4μm, HRA 91.0NegotiableMOQ: 10 Units
-
Polished Tungsten Carbide Hollow Rods for Precision Machining ApplicationsNegotiableMOQ: 1 Piece
-
Tungsten Carbide Saw Tips for TCT Circular Saw Blades and Woodworking CuttingNegotiableMOQ: 100 Pieces
-
Tungsten Carbide Gripper Inserts for Oilfield Slip Assemblies – YG8/YG6/K10 Grades, High Hardness & Wear ResistanceNegotiableMOQ: 5 Kilograms

-
Precision Carbide Sleeves OD 5-50 mm ID 2-30 mm Concentricity Max 0.005 mm Ra 0.2 um CNC GroundNegotiableMOQ: 1 Unit
-
Submicron Tungsten Carbide Strips 2x8x330mm Ground Tolerance ±0.02mm HRA 92.0NegotiableMOQ: 10 Pieces
-
VSI Crusher Carbide Strips and Bars for Machine Tool Plane Blades Wood Cutting ToolsNegotiableMOQ: 10 Units
-
Yg8 Standard Tungsten Carbide Tips Ss10 for Stone Cutting ToolsNegotiableMOQ: 5 Kilograms
-
Tungsten Carbide Circular Saw Blade for Slitting Slotting Flat Tooth Saw Blades Cutting Metal Stainless Steel Aluminium Custom OEM Factory Bulk PriceNegotiableMOQ: 1 Blade
-
Tungsten Carbide Woodworking Blades – Replacement Cutting Blades for Wood Carving, Trimming & Planing ToolsNegotiableMOQ: 1 Box
-
Custom Carbide Wear Components From Samples and Prototypes to Volume Production WC-Co SupplierNegotiableMOQ: 10 Blades
-
Custom Tungsten Carbide Wear Parts Non-Standard Shapes Produced to Customer Drawings WC-CoNegotiableMOQ: 10 Blades
-
Tungsten Carbide Strips and Plates PYG7 Submicron Grade M10 Ultra High Strength Custom SizesNegotiableMOQ: 10 Blades
-
Tungsten Carbide Strips and Plates PK08 Grade K30 High Strength Impact Resistant Custom SizesNegotiableMOQ: 10 Blades